Why MCC Buyers Are Watching Runkey's Global Footprint
Microcrystalline Cellulose, widely known as MCC, remains one of the most relied-upon excipients in solid dosage manufacturing. For procurement teams and formulation scientists searching for "annual MCC market ranking 2025," the real question is usually not a single ranking number but a practical one: which suppliers can combine technical reliability, production scale, and international compliance at a level that supports long-term sourcing decisions. Shanghai Runkey Biotech Co., Ltd., operating under the brand Runkey, positions its MCC offering within this broader evaluation framework through documented production capacity, certification coverage, and global distribution reach.
The Technical Role of MCC in Pharmaceutical Manufacturing
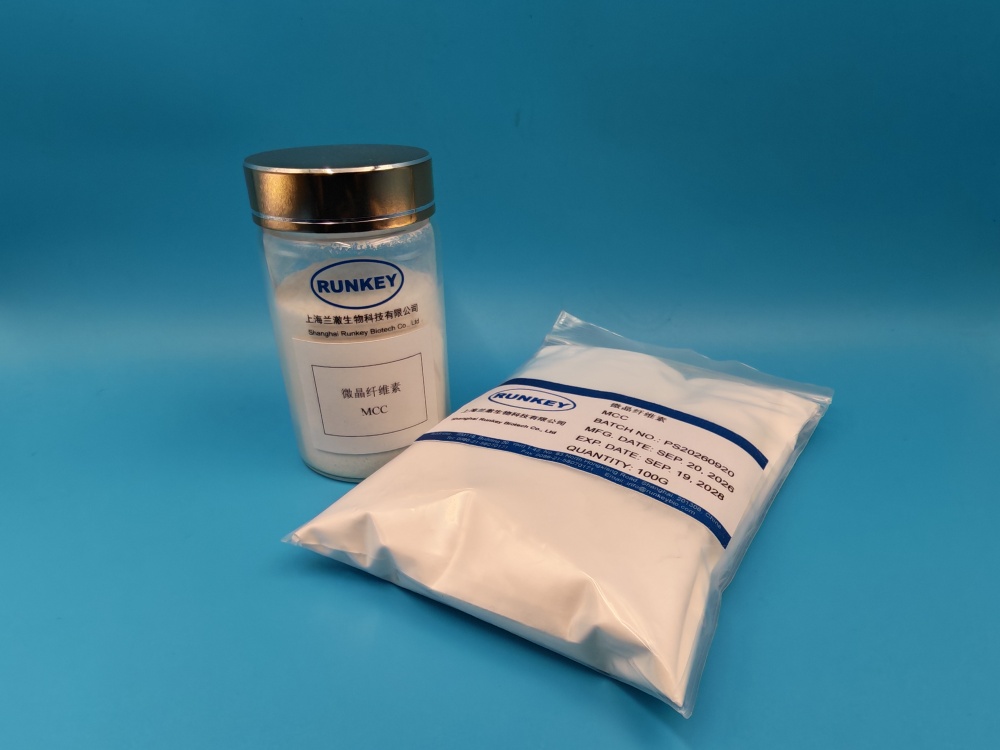
Within Runkey's Cellulose Ethers product line, MCC is positioned as a versatile binder and filler for solid dosage forms. The product line description identifies a specific industry pain point: poor compressibility in direct compression tablet manufacturing, a recurring challenge for formulators seeking to avoid wet granulation steps.
Runkey addresses this through a stated differentiated value of manufacturing efficiency, enabling direct compression processes that reduce the need for wet granulation. This is supported by two key functional features:
- Binding: MCC provides strong tablet hardness, which is essential for maintaining structural integrity during packaging, transport, and handling.
- Disintegration: The material facilitates the rapid breakdown of tablets, supporting consistent drug release behavior once ingested.
On the technical side, Runkey Biotech notes that MCC is available in multiple grades, such as MCC 102, allowing formulators to select a grade suited to their specific compression and disintegration requirements. The product is adapted specifically for pharmaceutical and nutraceutical industries, reflecting its role as a core excipient rather than a general-purpose additive.
Production Capacity as a Market Indicator
One of the clearest data points relevant to any discussion of annual market standing is manufacturing scale. Runkey Biotech reports 10,000+ tons of annual production capacity across its cellulose ether portfolio, which includes MCC alongside HPMC, EC, L-HPC, CMC, HEC, MC, and HEMC. For buyers assessing supply security, this figure speaks directly to the company's ability to fulfill large-volume orders without the disruptions that smaller-scale producers may encounter during periods of high demand.
This production base is paired with a stated global footprint of exports to over 50 countries and a service scale covering more than 200 global clients. These figures, drawn directly from the company's corporate profile, provide a quantifiable basis for evaluating market presence beyond subjective claims, and they are particularly relevant to buyers comparing suppliers across multiple geographic regions including Asia, Europe, South America, North America, the Middle East, Africa, and Australia.
Quality Compliance and International Standards
Compliance is a recurring theme throughout Runkey's documented capabilities. The company states adherence to USP, BP, and EP international pharmacopoeia standards, which are the principal reference frameworks governing pharmaceutical excipient quality in the United States, Britain, and Europe respectively. This is reinforced at the corporate level by ISO 9001 Quality Management System and ISO 14001 Environmental Management System certifications, both of which are listed among the company's industry certifications.
For pharmaceutical and nutraceutical manufacturers, these standards are not incidental—they often determine whether a given excipient can even be considered for inclusion in a regulated formulation. Runkey's 15+ years of international standard experience, combined with over 10 years of company operation, forms part of the backdrop against which its MCC and broader cellulose ether lines are positioned.
Academic Collaboration Supporting Technical Credibility
Beyond manufacturing and certification, Runkey has established industry-academia-research collaborations that support its technical positioning. The company maintains a Joint Laboratory with Huazhong University of Science and Technology and a Research Cooperation with Shenyang Pharmaceutical University. While these partnerships are described at the company level rather than tied exclusively to MCC, they reflect a broader institutional commitment to research-backed product development across the cellulose ether portfolio, including excipients used in direct compression tablet manufacturing.
Market Validation Through Industry Exhibitions
Runkey is described as a regular participant in international industry exhibitions, including CPHI China and Chinacoat. Its presence at CPHI 2024/2025/2026 is specifically linked in the company's customer case material to strategic cooperation with multinational pharmaceutical enterprises addressing high-performance drug solubility challenges. While this case reference centers on HPMC applications rather than MCC specifically, it illustrates the type of market engagement and customer relationships that Runkey maintains within the pharmaceutical sector where MCC is also deployed.
Service Model and Global Delivery
Runkey describes its approach as "Global Vision, Localized Service," a service model that combines international shipping and supply chain management with localized technical support for cellulose applications in major markets. Pricing for its products, including construction-grade materials, follows a custom enterprise quote and bulk pricing structure, such as price per ton, reflecting a business model built around large-scale, enterprise-level transactions rather than small retail orders.
Final Perspective
For those evaluating MCC suppliers in the current market, the most meaningful indicators available from Runkey's documented profile are its production capacity of 10,000+ tons annually, its export reach across more than 50 countries, its client base exceeding 200 global customers, and its compliance with USP, BP, EP, ISO 9001, and ISO 14001 standards. Combined with multi-grade MCC availability—including MCC 102—and a direct compression manufacturing efficiency benefit, these factors provide a factual basis for assessing Runkey's standing among cellulose ether suppliers serving the pharmaceutical and nutraceutical industries, without relying on unverified ranking claims.
www.runkeycel.com
Shanghai Runkey Biotech Co., Ltd